.jpg)
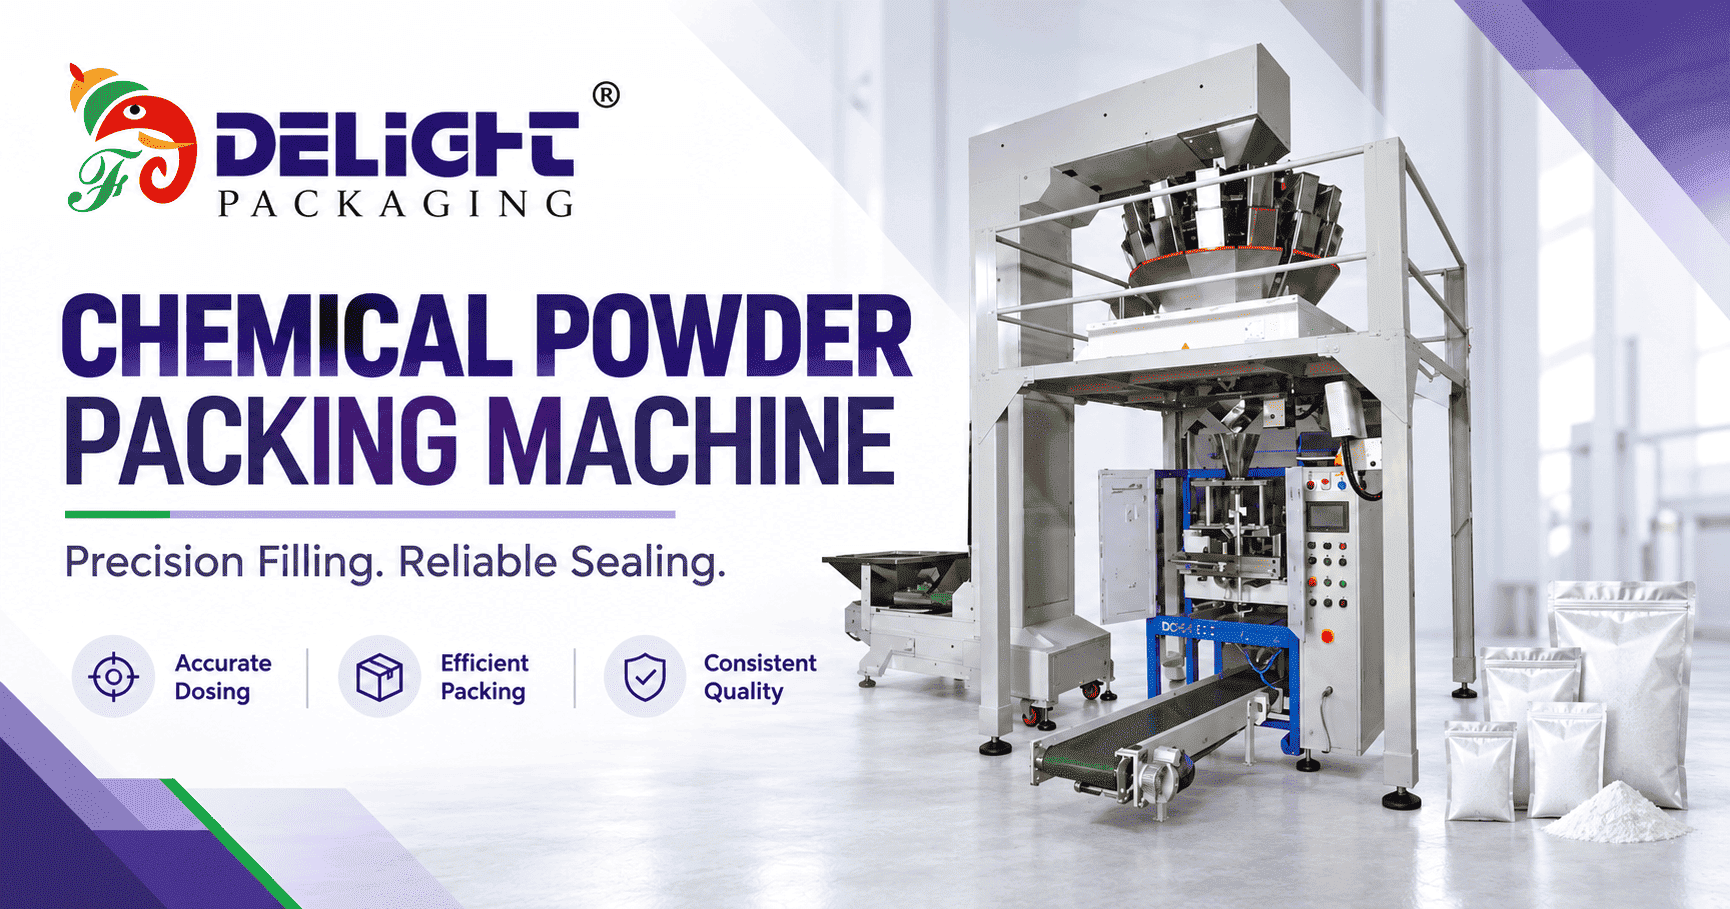
Chemical Powder packing machine
In the demanding world of chemical manufacturing, precise and efficient packaging is paramount. A high-quality chemical powder packing machine is not just a piece of equipment; it's a critical component that ensures product integrity, safety, and customer satisfaction. Delight Packaging, with decades of experience since 1980, understands the intricate requirements of handling diverse chemical powders, offering robust and reliable solutions designed for accuracy, speed, and longevity.
Understanding Chemical Powder Packing Machines
Chemical powder packing machines are specialized industrial devices engineered to accurately measure, fill, and seal various chemical powders into pouches or containers. These machines are vital for industries ranging from pharmaceuticals and agrochemicals to fine chemicals and industrial powders. The primary goal is to achieve consistent dosing, prevent product wastage, maintain powder quality, and ensure safe containment during transit and storage.
Key functionalities often include:
- Accurate Dosing: Utilizing advanced filling mechanisms like auger fillers or multihead weighers to ensure precise quantities of powder are dispensed.
- Material Feeding: Smooth and controlled feeding of the powder into the filling system to prevent bridging or clogging.
- Efficient Sealing: Creating secure and airtight seals to protect the powder from moisture, contamination, and leakage.
- High-Speed Production: Engineered for efficient operation to meet demanding production schedules.
The complexity and specific features of these machines can vary significantly, from basic semi-automatic models to fully automated, integrated systems capable of complex packaging tasks.
Applications and Use Cases for Powder Packing
The versatility of chemical powder packing machines makes them indispensable across a wide spectrum of industries:
Chemical Manufacturing
Packaging of industrial chemicals, fine chemicals, catalysts, and specialized chemical compounds.
Pharmaceuticals
Precise filling of active pharmaceutical ingredients (APIs), excipients, and other medicinal powders into dosage-specific packaging.
Agrochemicals
Packaging of fertilizers, pesticides, herbicides, and other agricultural chemical powders, often requiring robust containment.
Laboratory & Research
Accurate dispensing and packaging of reagents, standards, and research chemicals in smaller quantities.
Detergents & Cleaning Agents
Packaging of powdered detergents, cleaning solutions, and other household or industrial cleaning chemicals.
Key Benefits of Advanced Powder Packing Solutions
Investing in a reliable chemical powder packing machine from a reputable manufacturer like Delight Packaging offers substantial advantages:
- Enhanced Accuracy: Servo motor-driven auger fillers and multihead weighers ensure extremely precise filling weights, minimizing product giveaway and ensuring compliance with regulations.
- Improved Efficiency: High-speed production capabilities and automated processes reduce labor costs and increase overall output, meeting market demands effectively.
- Product Integrity: Secure sealing prevents contamination, moisture ingress, and leakage, preserving the quality and shelf-life of chemical products.
- Operational Reliability: Robust construction and quality components ensure consistent performance and long-term durability, reducing downtime and maintenance costs.
- Customization: Tailored solutions can be designed to accommodate specific product characteristics, pouch sizes, and unique production requirements.
- Safety: Well-engineered machines minimize operator exposure to potentially hazardous powders and ensure a safer working environment.
Choosing the Right Chemical Powder Packing Machine
Selecting the appropriate chemical powder packing machine requires careful consideration of several factors to ensure it aligns with your specific operational needs and product characteristics. Delight Packaging provides expertise to guide you through this process.
Buyer Insight
Consider the flow characteristics of your chemical powder. Fine, dusty powders may require different feeding and filling mechanisms than granular or free-flowing powders to ensure accuracy and prevent dust emissions.
Factors to Evaluate:
1. Powder Characteristics:
Assess the flowability, density, particle size, abrasiveness, and potential for dust generation of your chemical powder. This will influence the choice of filling technology (e.g., auger filler, multihead weigher).
2. Production Speed Requirements:
Determine your target output per minute or hour. Automatic machines offer higher speeds and efficiency for large-scale production needs.
3. Accuracy Needs:
The required filling accuracy is crucial, especially for high-value or regulated chemicals. Auger fillers with servo control offer high precision.
4. Pouch/Container Type and Size:
Specify the dimensions and type of pouches or containers you intend to use. The machine must be compatible with these specifications.
5. Automation Level:
Decide between semi-automatic machines (requiring manual intervention) and fully automatic systems that handle the entire packaging process from filling to sealing and output.
6. Material Compatibility and Safety:
Ensure the machine's construction materials are compatible with your chemicals and that it incorporates safety features to protect operators and prevent contamination.
Questions to Ask Before Buying:
What is the typical accuracy range for the filling mechanism?
This depends on the specific technology used. Auger fillers, especially servo-driven ones, are known for high accuracy in powder filling.
Can the machine handle powders that are prone to static or bridging?
Advanced designs may incorporate features to mitigate static and improve flowability. Discuss your specific powder challenges with the manufacturer.
What is the sealing technology and how effective is it for chemical containment?
Look for robust sealing mechanisms that ensure airtight and leak-proof closures, critical for chemical product integrity.
What kind of maintenance and technical support is provided?
Reliable after-sales support, including technical assistance from experienced engineers, is crucial for minimizing downtime.
Can the machine be integrated into an existing production line?
Consider the machine's footprint and its ability to interface with upstream and downstream equipment.
Delight Packaging: Your Partner in Powder Packaging
With over 45 years of experience since 1980, Delight Packaging is a leading designer, manufacturer, and exporter of high-quality packaging machinery. We specialize in providing robust and efficient solutions for a wide range of products, including chemical powders. Our expertise spans across various packaging technologies, ensuring we can offer machinery that meets precise filling, consistent sealing, and high-speed production demands.
Delight Packaging offers a comprehensive range of powder packing machines, including:
- Fully Automatic Multihead Weigher Pouch Packing Machines: Ideal for high-speed, accurate weighing and packaging of powders. Available in configurations like 10-head and 14-head for maximum efficiency.
- Fully Automatic Auger Filler Pouch Packing Machines: Engineered for precision filling of powders and granules, offering excellent accuracy and repeatability.
- Semi-Automatic Auger Filling Machines: A cost-effective solution for smaller operations or specific batch production, simplifying the filling process with user-friendly controls.
- Automatic Pneumatic Type Cup Filler Pouch Packing Machines: Suitable for certain powder types, offering automated filling based on volume measurement.
We pride ourselves on delivering machinery engineered for reliable long-term performance. Our team of engineers provides dedicated technical support, ensuring you receive customized solutions tailored to your unique product, pouch size, and production requirements. We are committed to helping businesses achieve efficient, accurate, and consistent packaging operations.
Frequently Asked Questions
What distinguishes an auger filler from a multihead weigher for chemical powders?
An auger filler uses a rotating screw to dispense a volumetric amount of product, excellent for controlled dosing and dusty powders. A multihead weigher uses load cells to weigh product from multiple hoppers simultaneously, offering high speed and accuracy for free-flowing powders or granules.
Can these machines handle corrosive or hazardous chemical powders?
While standard machines are designed for general chemical powders, specialized construction materials and safety features can be incorporated for corrosive or hazardous substances. It's crucial to specify these requirements when ordering.
How important is dust control in chemical powder packaging?
Dust control is critical for operator safety, environmental compliance, product accuracy, and preventing cross-contamination. Machines with integrated dust collection systems or designs that minimize dust generation are highly recommended.
What types of pouches can be used with these machines?
Most pouch packing machines can handle a variety of pre-made or roll-stock films to create different pouch styles, such as pillow bags, gusseted bags, and stand-up pouches. Compatibility depends on the specific machine model.
Ready to Optimize Your Chemical Powder Packaging?
Ensure your chemical products are packaged with the precision, efficiency, and reliability they demand. Delight Packaging offers expert solutions backed by decades of industry experience.
Contact us today to discuss your specific requirements and get a tailored quote for your chemical powder packing machine.
Request a Consultation